- Whatsapp: 8613738300923
- Email: [email protected]


Choosing a reliable stainless steel ball valve factory is essential for ensuring product quality, operational safety, and long-term performance in industrial piping systems. Stainless steel ball valves are widely used in oil and gas, chemical processing, water treatment, food and beverage production, pharmaceutical manufacturing, and other industries where reliable flow control is required.
However, not all manufacturers follow the same quality management procedures or product testing requirements. A qualified factory should have effective quality control systems, use suitable materials, maintain dimensional accuracy, and conduct appropriate performance tests before shipment. Understanding the relevant quality standards helps buyers evaluate manufacturers more effectively and select products that meet their application requirements.
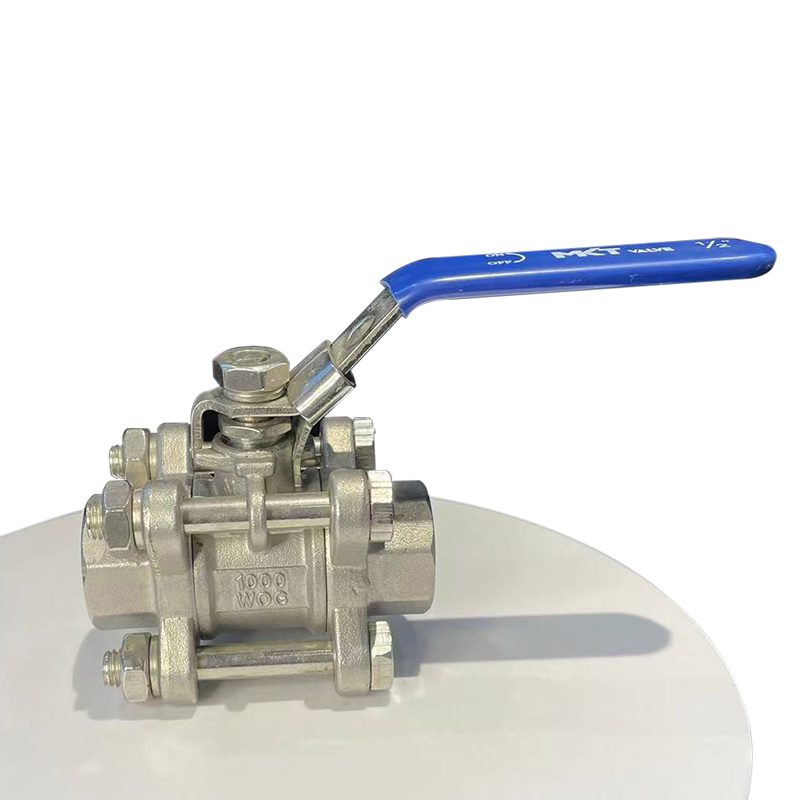
ISO 9001 is an internationally recognized standard for quality management systems. For a stainless steel ball valve factory, certification can demonstrate that the company has established procedures for managing production processes, monitoring product quality, handling customer requirements, and improving operational performance.
A manufacturer with a well-implemented quality management system should maintain inspection records, control nonconforming products, manage supplier quality, and establish procedures for corrective actions. These practices help reduce manufacturing inconsistencies and improve product traceability.
Buyers should verify the validity and scope of a factory’s ISO 9001 certificate rather than relying solely on a logo displayed on its website. Certification is useful evidence of a structured quality system, but it does not automatically guarantee that every valve meets the required technical specifications.
Material quality directly affects a ball valve’s corrosion resistance, mechanical strength, durability, and suitability for different operating environments. Common stainless steel grades include 304, 316, and 316L, although the appropriate grade depends on the valve design and the service conditions.
ASTM material specifications are frequently used to define the chemical composition and mechanical properties of stainless steel components. For example, ASTM A351 covers castings made from austenitic steel for pressure-containing parts, while ASTM A182 covers forged or rolled alloy and stainless steel pipe flanges, forged fittings, and valves and parts for high-temperature service.
A reliable factory should be able to identify the material specifications applicable to its products and provide material test certificates when required. Buyers should also confirm that the specified grade applies to the relevant components, including the valve body, ball, and stem, rather than assuming that every part uses the same stainless steel.
For corrosive environments, 316 or 316L may be more suitable than 304 because of their molybdenum content. Nevertheless, material selection must consider the actual medium, concentration, temperature, and operating conditions.
Stainless steel ball valves must be manufactured according to appropriate design and dimensional requirements. These requirements help ensure compatibility with piping systems, reliable operation, and suitable pressure-containing performance.
Several standards may be relevant depending on the valve type and intended application:
API 608: Covers metal ball valves with flanged, threaded, and welding ends for applicable industrial services.
ASME B16.34: Addresses valve pressure-temperature ratings, materials, dimensions, testing, and other design requirements within its scope.
ISO 17292: Specifies requirements for metal ball valves used in petroleum, petrochemical, and related industries.
ASME B16.10: Covers face-to-face and end-to-end dimensions for certain valve types and configurations.
Not every stainless steel ball valve needs to comply with all these standards. The applicable requirements depend on its design, connection type, pressure rating, industry, and purchasing specifications.
A qualified factory should clearly identify which standards apply to each product series and ensure that drawings, materials, machining tolerances, assembly procedures, and inspection plans are consistent with those requirements.
Pressure testing is an important part of ball valve quality control. It helps verify pressure-containing integrity and assess whether the valve meets the specified leakage acceptance criteria.
Common testing references include API 598 and ISO 5208. These standards address inspection and testing requirements for industrial valves, including applicable shell tests, closure tests, and leakage criteria.
A typical valve testing process may include shell pressure testing to check the pressure boundary and closure testing to evaluate sealing performance when the valve is closed. The required test medium, pressure, duration, and acceptance criteria depend on the applicable standard, valve design, pressure rating, and purchase requirements.
Buyers should ask whether the factory conducts testing on every valve or uses a sampling-based inspection plan. They should also confirm whether test records can be provided for the order. A pressure test certificate or inspection report can help demonstrate compliance with the agreed requirements, but its value depends on the accuracy and traceability of the recorded results.
Even when a valve uses the correct stainless steel grade, dimensional inconsistencies can cause installation difficulties, operating problems, or sealing failures. Manufacturing accuracy is therefore another important factor when evaluating a stainless steel ball valve factory.
Critical dimensions may include the valve’s face-to-face length, connection dimensions, bore diameter, ball geometry, stem dimensions, and sealing surfaces. These dimensions should be inspected against approved drawings and the applicable product standards.
Precision machining is particularly important for the ball and sealing surfaces. Poor surface finish, excessive dimensional variation, or incorrect assembly can increase operating torque and affect sealing performance.
A capable manufacturer should use appropriate measuring instruments, maintain calibration records, and establish inspection procedures for critical components. Buyers requiring customized valves should confirm dimensional tolerances and acceptance criteria before production begins.
A stainless steel ball valve is an assembly of multiple components, and its overall performance depends on how well these parts work together. In addition to the body and ball, important components include the stem, seats, stem packing, gaskets, and operating mechanism.
Common seat materials include PTFE and other engineered polymers, depending on the required chemical compatibility, temperature range, pressure conditions, and sealing performance. The factory should select materials according to the intended service rather than using a standard configuration for every application.
Stem design and packing quality are also important because they influence external leakage control and operating reliability. For demanding services, buyers may need to specify fire-safe design, antistatic features, emissions requirements, or other application-specific provisions.
The manufacturer should document the relevant component specifications and verify that the selected materials are compatible with the process medium and expected operating conditions.
Traceability helps buyers identify the materials, production processes, and inspection results associated with a particular valve or order. It is especially important for industrial projects that require documented quality assurance or future maintenance support.
Depending on the product and contract requirements, traceability records may include material certificates, heat or batch numbers, machining and assembly records, pressure test reports, final inspection results, and product identification markings.
A factory with effective traceability procedures should be able to connect the required documentation to the supplied products. This makes it easier to investigate quality issues, verify material compliance, and manage replacement parts.
Before placing a bulk order, buyers should clarify which documents will be supplied, how products will be marked, and whether inspection records can be linked to individual valves or production batches.
Some applications require additional compliance measures beyond general manufacturing quality standards. For example, valves used in food processing, pharmaceutical production, hazardous environments, or regulated industrial facilities may be subject to specific material, hygiene, safety, or regulatory requirements.
For equipment intended for European markets, applicable CE marking obligations must be assessed according to the product’s design, pressure classification, intended use, and relevant legislation. CE marking should not be treated as a universal quality certificate for all ball valves.
For fire-safe applications, buyers may need to check whether the valve design has been tested to a relevant standard, such as API 607 or API 6FA, where applicable. These standards address fire testing for specified valve designs and configurations.
A responsible factory should explain which certifications, test reports, or declarations apply to its products and provide supporting documentation when required. Buyers should verify the scope of any certification and ensure that it covers the actual model being purchased.
When comparing manufacturers, buyers should evaluate the complete quality assurance process rather than focusing on price or certification alone. A practical supplier assessment should cover material control, manufacturing capabilities, testing procedures, documentation, and order management.
Before placing an order, consider asking the factory the following questions:
Which design, material, and testing standards does the product comply with?
Can the factory provide material certificates and pressure test reports?
Are critical dimensions inspected against approved drawings?
How are nonconforming products identified and controlled?
What traceability information is available for each order?
Can the factory support customized designs, pressure ratings, and connection types?
Are third-party inspections or customer witness tests available when required?
It is also useful to request technical drawings, product datasheets, inspection plans, and sample documentation before confirming a purchase. For large or critical orders, buyers may consider an independent inspection to verify that the supplied products meet the agreed specifications.
A reliable stainless steel ball valve factory should combine an effective quality management system with appropriate material control, standardized manufacturing procedures, pressure testing, dimensional inspection, and product traceability. Relevant standards such as ISO 9001, ASTM material specifications, API 598, ISO 5208, API 608, and ASME B16.34 can help buyers establish clear quality requirements, depending on the product and application.
However, no single certificate or standard is sufficient to evaluate every aspect of valve quality. Buyers should confirm the applicable requirements for their operating conditions and verify that the manufacturer can provide supporting technical documentation and inspection records.
By evaluating these factors before purchasing, distributors, engineering contractors, and industrial end users can make more informed sourcing decisions and establish more reliable long-term supplier relationships.
1. What quality standards should a stainless steel ball valve factory meet?
A stainless steel ball valve factory should maintain an effective quality management system, such as ISO 9001, and follow applicable material, design, manufacturing, and testing standards. Depending on the valve type and application, relevant standards may include ASTM material specifications, API 598, API 608, ISO 5208, and ASME B16.34.
2. Is ISO 9001 certification important for a stainless steel ball valve manufacturer?
Yes. ISO 9001 certification demonstrates that a manufacturer has established a quality management system for controlling processes, monitoring product quality, and improving operational performance. However, buyers should also evaluate product-specific testing procedures, technical capabilities, and inspection records.
3. How does a factory ensure the quality of stainless steel ball valves?
A factory can ensure quality through material verification, precision machining, dimensional inspection, controlled assembly, pressure testing, and final inspection. Maintaining traceable production records and addressing nonconforming products are also important for consistent product quality.
4. What tests should stainless steel ball valves undergo before shipment?
Common tests include shell pressure testing, closure leakage testing, dimensional inspection, and operational checks. The exact testing requirements depend on the valve design, applicable standards, pressure rating, and customer specifications.
5. Which stainless steel grades are commonly used for ball valves?
Common grades include 304, 316, and 316L stainless steel. Grade 304 is suitable for many general applications, while 316 and 316L often provide improved resistance to certain corrosive environments. The final selection should consider the process medium, temperature, pressure, and service conditions.
6. What documents should buyers request from a stainless steel ball valve factory?
Buyers may request material test certificates, product datasheets, technical drawings, pressure test reports, dimensional inspection records, and applicable quality certificates. For specialized applications, additional compliance documents or third-party inspection reports may be necessary.
STAINLESS STEEL&GENCEL;
Privacy Policy | SiteMap
Copyright GENCEL STAINLESS STEEL CO.,LIMITED
 Optimized by Seraphinite Accelerator