- Whatsapp: 8613738300923
- Email: [email protected]


Butt welded pipe fittings are essential components in industrial piping systems, used to change flow direction, connect pipe branches, reduce pipe diameter, and close pipeline ends. They are widely applied in oil and gas, chemical processing, power generation, water treatment, shipbuilding, and other industries that require reliable pipe connections.
Unlike detachable connections, butt weld fittings are joined directly to pipes through welding, creating a permanent connection when properly designed and installed. Their performance depends on material quality, manufacturing precision, dimensional accuracy, welding preparation, and compliance with applicable technical standards.
For manufacturers, engineers, distributors, and purchasing teams, understanding how butt welded pipe fittings are manufactured and inspected helps reduce quality risks and improve piping system reliability. This guide explains the main manufacturing processes, relevant quality standards, and inspection methods used to evaluate these components.
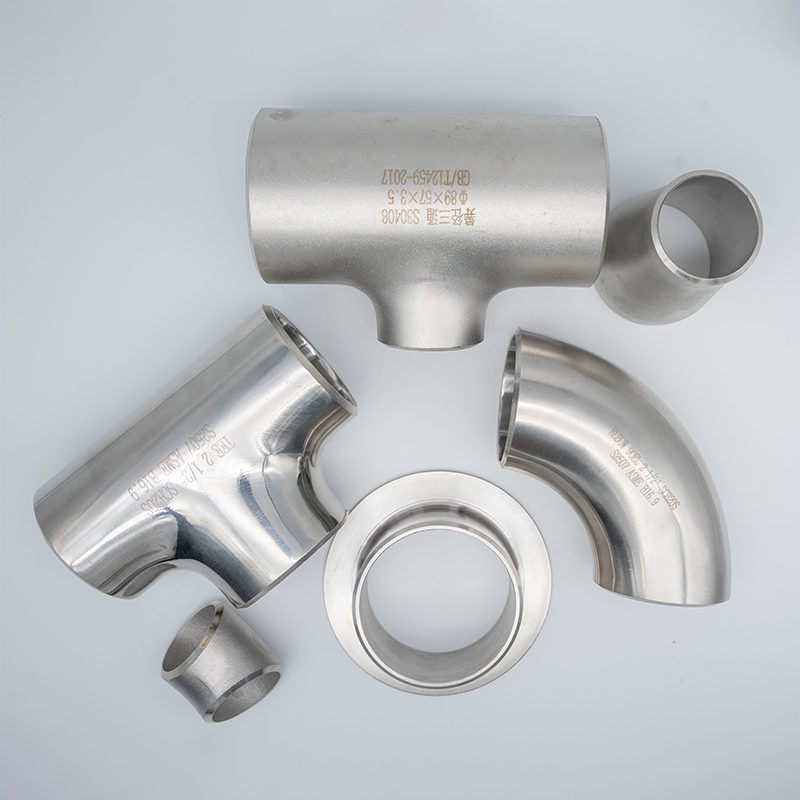
Butt welded pipe fittings are pipe components designed to be connected to pipes by welding their prepared ends together. The fitting ends are generally aligned with the pipe ends, and the joint is welded to form a continuous connection.
Common types include butt weld elbows, tees, reducers, and caps. Elbows change the direction of flow, tees create branch connections, reducers connect pipes of different diameters, and caps close the ends of pipelines.
These fittings are available in various materials, including carbon steel, stainless steel, alloy steel, and other materials selected according to operating conditions. They also come in different sizes, wall thicknesses, and configurations to accommodate piping design requirements.
Butt welded connections are commonly selected for systems requiring permanent joints, structural integrity, and reliable performance under specified pressure and temperature conditions. However, actual performance depends on the fitting design, material, welding procedure, installation quality, and operating environment.
The manufacturing process varies according to the fitting type, material, size, wall thickness, and applicable standard. A typical production workflow includes raw material preparation, forming, heat treatment where required, machining, surface finishing, and inspection.
Manufacturing begins with selecting suitable raw materials, such as steel plate, pipe, tube, or other permitted starting forms. The material must meet the chemical composition and mechanical property requirements specified for the finished fitting.
Manufacturers review material certificates and may perform additional verification when required by the order or quality plan. Material identification and traceability help ensure that the correct grade is used throughout production.
Before forming, the raw material is cut to the required dimensions. Cutting accuracy and material condition can affect subsequent forming operations and the final fitting geometry.
Different fitting types require different forming methods.
Butt Weld Elbows: Elbows may be manufactured using hot forming, cold forming, or other qualified processes. The selected method shapes the material into the required angle and curvature while controlling wall thickness and dimensional accuracy.
Butt Weld Tees: Tees may be produced through methods such as extrusion, hydraulic forming, or other suitable forming processes. The manufacturing method must provide the required branch geometry and material integrity.
Butt Weld Reducers: Reducers are commonly formed by processes such as pressing or spinning, depending on their dimensions, material, and design. The process creates a transition between different pipe diameters.
Butt Weld Caps: Caps may be formed from plate or other suitable starting materials using pressing, dishing, or related processes. The finished shape must meet the specified dimensions and wall thickness requirements.
Forming parameters should be controlled to prevent defects such as excessive thinning, wrinkles, cracks, and unacceptable distortion. The appropriate process depends on the product specification and material characteristics.
Heat treatment may be required after forming to achieve the specified mechanical properties, relieve residual stresses, or address material-specific manufacturing requirements.
The applicable treatment depends on the material grade, forming temperature, product dimensions, governing standard, and purchase specification. Not every fitting requires the same heat treatment, and some manufacturing routes may not require a separate treatment under particular conditions.
When heat treatment is specified, manufacturers should control the process parameters and maintain the required records. Temperature monitoring, treatment duration, cooling conditions, and traceability may all be important for verifying process conformity.
After forming and any required heat treatment, fittings may undergo machining to achieve the specified dimensions and end geometry.
For butt welded fittings, end preparation is especially important. Welding ends may require a bevel or another specified profile to support proper joint preparation and weld penetration.
Manufacturers also verify critical dimensions such as outside diameter, wall thickness, center-to-end dimensions, overall length, and fitting angle. Dimensional deviations can complicate pipe alignment and affect installation quality.
Surface finishing removes unwanted scale, burrs, or other surface irregularities when required. Depending on the material and specification, finishing may involve pickling, blasting, grinding, or other suitable treatments.
Stainless steel fittings may require particular attention to surface contamination and corrosion resistance. Carbon steel fittings may require protective coatings or temporary corrosion protection depending on storage and delivery conditions.
Product marking typically identifies relevant information such as material grade, size, wall thickness or schedule, manufacturer, heat or batch number, and applicable standard where required. Clear identification supports traceability during inspection, storage, and installation.
Quality standards define requirements for dimensions, materials, manufacturing, testing, and product acceptance. The appropriate standard depends on the fitting type, material, piping design, application, and destination market.
Several standards are commonly relevant to butt welded pipe fittings.
ASME B16.9: Covers factory-made wrought butt welding fittings, including specified dimensions, tolerances, ratings, testing, and marking requirements. It is widely referenced for fittings used in industrial piping systems.
ASME B16.25: Addresses butt welding ends, including end preparation requirements that affect the fit-up and welding of piping components.
ASTM A234/A234M: Covers wrought carbon steel and alloy steel piping fittings intended for use at moderate and elevated temperatures, within the scope of the specification.
ASTM A403/A403M: Covers wrought austenitic stainless steel piping fittings, including specified material and manufacturing requirements.
EN 10253: A European series of standards covering butt-welding pipe fittings. The applicable part depends on the product type, material, and relevant technical requirements.
These standards are not interchangeable in every situation. Buyers should identify the exact standard and edition required by the project and confirm that the manufacturer can supply the specified fitting type, material grade, dimensions, and documentation.
It is also important to distinguish product standards from quality management certifications. For example, ISO 9001 relates to a quality management system; it does not, by itself, demonstrate that a particular fitting complies with ASME B16.9, ASTM A234/A234M, or another product specification.
Quality assessment involves more than checking whether a fitting looks correct. Several technical characteristics can affect its suitability for installation and service.
The material must meet the specified chemical composition and mechanical property requirements. Depending on the material and applicable specification, relevant properties may include tensile strength, yield strength, elongation, hardness, and impact toughness.
Material verification helps prevent the use of an incorrect grade or an unsuitable material for the intended operating conditions. For applications requiring traceability, the fitting should be linked to the relevant material documentation and production records.
Dimensions must comply with the applicable standard and purchase specification. Important characteristics include outside diameter, wall thickness, center-to-end dimensions, branch dimensions, overall length, and end bevel geometry.
Incorrect dimensions may create alignment difficulties during installation, require additional adjustment, or affect the fit-up of welded joints. Wall thickness is particularly important because it must be suitable for the specified piping design and service conditions.
The fitting surface should meet the specified acceptance criteria. Depending on the material and product requirements, inspectors may check for cracks, laps, seams, excessive scale, corrosion, dents, and other unacceptable surface conditions.
Not every surface mark indicates a defect, so acceptance should be based on the applicable specification and inspection criteria rather than appearance alone.
The forming process must preserve the required material integrity. Defects such as cracks, unacceptable wall thinning, or significant deformation may affect the fitting’s suitability for service.
The required inspection and testing methods depend on the product standard, material, manufacturing route, service conditions, and project requirements. Additional examinations may be necessary for critical piping applications.
Inspection helps verify whether the finished fittings comply with the agreed specifications. Manufacturers may perform inspections at different production stages, including incoming material inspection, in-process inspection, and final inspection.
Visual inspection is used to identify visible defects, surface damage, forming irregularities, corrosion, and marking errors. Inspectors may also examine the condition of welding ends and verify that the product is clean and properly protected.
Visual inspection is useful for identifying obvious problems but cannot detect every internal or subsurface defect.
Dimensional inspection verifies that the fitting matches the required geometry and tolerances. Depending on the fitting, tools may include calipers, micrometers, measuring tapes, gauges, templates, and other suitable instruments.
Typical inspection points include outside diameter, wall thickness, center-to-end dimensions, branch alignment, angle, overall length, and end bevel dimensions.
For orders with strict dimensional requirements, buyers should agree on the inspection points, sampling plan, and acceptance criteria before production begins.
Material verification confirms that the fitting uses the specified material grade. Methods may include reviewing material test certificates, checking heat numbers, and performing material identification tests where required.
Positive material identification (PMI) may be used to verify alloy composition in applicable situations. However, PMI alone does not replace all required material testing or demonstrate compliance with every mechanical property requirement.
Non-destructive testing (NDT) methods may be used to detect defects without damaging the component. The required method depends on the material, manufacturing process, potential defect type, and applicable specification.
Common methods include:
Ultrasonic Testing (UT): Uses sound waves to detect certain internal discontinuities and evaluate material conditions within the method’s limitations.
Radiographic Testing (RT): Uses X-rays or gamma rays to reveal certain internal discontinuities in suitable components.
Magnetic Particle Testing (MT): Detects surface and near-surface discontinuities in ferromagnetic materials.
Liquid Penetrant Testing (PT): Helps identify surface-breaking discontinuities in nonporous materials.
These methods are not mandatory for every butt weld fitting. Inspection scope, coverage, acceptance criteria, and personnel qualification requirements should follow the applicable standard, purchase order, or project inspection plan.
Mechanical tests may be required to verify specified material properties. Depending on the material and product specification, these may include tensile, hardness, impact, or other tests.
Hydrostatic or other pressure-related testing should not be assumed to be a universal requirement for every butt weld fitting. Such testing depends on the governing product specification, design requirements, and purchaser agreement. Where applicable, the test method and acceptance criteria should be clearly defined.
Selecting a capable manufacturer is important for maintaining consistent product quality and meeting delivery requirements. Buyers should assess technical competence, manufacturing controls, inspection capabilities, and documentation practices.
First, confirm the manufacturer’s experience with the required fitting types, material grades, sizes, and wall thicknesses. A supplier may specialize in certain materials or dimensions, so production capability should be verified against the project specification.
Second, review the quality management process. Ask how raw materials are identified, forming processes are controlled, heat treatment is documented where required, and finished products are inspected. If the order requires NDT or special testing, confirm whether these services are performed in-house or by qualified external providers.
Third, check the manufacturer’s documentation capabilities. Depending on the order, relevant documents may include material test certificates, dimensional inspection reports, heat treatment records, NDT reports, and a certificate of conformity.
Finally, evaluate production capacity, lead times, packaging, communication, and the ability to support repeat orders. A clear purchasing specification and agreed inspection plan can help reduce misunderstandings between the buyer and manufacturer.
Pre-shipment quality checks can help buyers identify discrepancies before the products leave the factory. The inspection process should be agreed upon before production and should reflect the product specification and application risks.
A typical pre-shipment inspection may cover product type and quantity, material identification, dimensions, surface condition, end preparation, marking, documentation, and packaging. For critical applications, additional testing or third-party inspection may be specified.
Buyers should also confirm that product markings match the purchase order and supporting certificates. Traceability records are particularly important when several material grades, heat numbers, or product sizes are included in the same shipment.
Packaging should protect fittings from impact, contamination, moisture, and corrosion during transportation. Suitable separators, end protection, and clear identification can help preserve product condition and simplify receiving inspections.
For repeat orders, maintaining approved drawings, material requirements, inspection records, and acceptance criteria helps improve consistency across production batches.
Butt welded pipe fittings are important components in industrial piping systems, and their performance depends on appropriate materials, controlled manufacturing processes, dimensional accuracy, and compliance with relevant product standards.
Manufacturing may involve material preparation, forming, heat treatment where required, machining, end preparation, and surface finishing. Quality verification may include visual and dimensional inspection, material verification, non-destructive testing, and other tests specified by the applicable requirements.
For buyers, understanding these processes makes it easier to assess supplier capabilities and establish practical quality requirements. By confirming the governing standards, material specifications, inspection scope, and documentation before placing an order, businesses can reduce sourcing risks and obtain butt weld fittings suited to their intended applications.
1. What are butt welded pipe fittings?
Butt welded pipe fittings are piping components connected to pipes by welding their beveled ends together. Common types include elbows, tees, reducers, and caps, which help change flow direction, connect branches, adjust pipe diameter, or close pipe ends.
2. What materials are used to manufacture butt welded pipe fittings?
Common materials include carbon steel, stainless steel, and alloy steel. The appropriate material depends on the working medium, operating temperature, pressure, corrosion resistance requirements, and applicable industry standards.
3. What standards apply to butt welded pipe fittings?
Common standards include ASME B16.9 for factory-made wrought butt welding fittings, ASME B16.25 for butt-welding ends, ASTM A234/A234M for carbon and alloy steel fittings, and ASTM A403/A403M for wrought austenitic stainless steel fittings. Requirements vary by material and application.
4. How are butt welded pipe fittings manufactured?
The manufacturing process typically involves raw material inspection, cutting, forming, heat treatment when required, machining, end beveling, surface finishing, marking, and final inspection. Specific processes depend on the fitting type, material, dimensions, and applicable standard.
5. How do you inspect the quality of butt welded pipe fittings?
Quality inspection may include visual examination, dimensional checks, material verification, mechanical testing, and non-destructive testing (NDT). Methods such as ultrasonic testing, radiographic testing, magnetic particle testing, and liquid penetrant testing are selected according to the product specification and inspection requirements.
STAINLESS STEEL&GENCEL;
Privacy Policy | SiteMap
Copyright GENCEL STAINLESS STEEL CO.,LIMITED
 Optimized by Seraphinite Accelerator