- Whatsapp: 8613738300923
- Email: [email protected]


Bolted clamps are widely used in industrial applications to secure pipes, hold components in position, support equipment, and maintain stable connections. Their performance depends on several factors, including material quality, structural design, dimensional accuracy, bolt strength, and manufacturing consistency.
For industrial buyers, understanding how bolted clamps are manufactured and quality tested helps with supplier evaluation and product selection. A reliable manufacturing process ensures that each component meets the specified dimensions and assembly requirements, while appropriate quality inspections help identify defects before products are delivered.
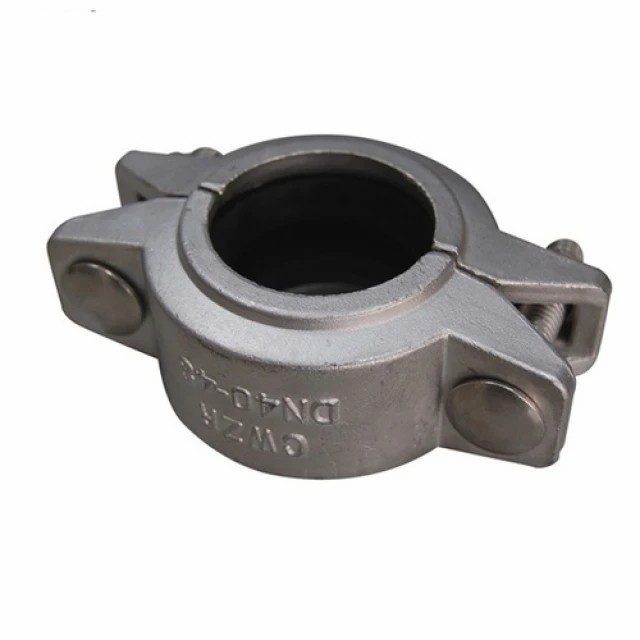
Material selection is the first step in bolted clamp manufacturing. The appropriate material depends on the clamp’s intended application, required load capacity, operating environment, and exposure to moisture, chemicals, or temperature changes.
Stainless steel is commonly selected for applications requiring corrosion resistance and durability. Grades such as 304 and 316 stainless steel are used in different industrial environments. Grade 316 generally offers better resistance to pitting and crevice corrosion in chloride-containing environments than grade 304, although actual performance depends on service conditions.
Carbon steel may be suitable for applications requiring mechanical strength and cost-effective production. Depending on the environment, carbon steel clamps may require galvanizing, plating, painting, or another protective surface treatment to reduce corrosion.
Manufacturers should verify incoming materials against the relevant specifications. Material certificates, grade identification, and traceability records can help confirm that the raw materials meet the customer’s requirements.
After material selection, raw materials are prepared for processing. Depending on the clamp design, manufacturing may involve cutting metal sheets, bars, plates, or other stock materials into the required sizes.
The clamp body is then formed or machined according to the product drawing. Common processes include bending, stamping, forging, casting, or CNC machining, depending on the structure, material, production volume, and required precision.
During forming, manufacturers must control dimensions and geometry to ensure that the clamp fits the intended pipe, component, or mounting surface. Uneven forming, excessive deformation, or inconsistent dimensions can affect assembly and load distribution.
For custom bolted clamps, production drawings should clearly define the clamp dimensions, material thickness, hole positions, mounting requirements, and tolerances before manufacturing begins.
Bolted clamps typically require holes or threaded features to accommodate bolts and other fastening components. These features may be produced through drilling, punching, tapping, or machining, depending on the design.
Hole diameter, spacing, alignment, and edge quality are important because they affect bolt installation and the fit between mating components. Misaligned holes can make assembly difficult, while damaged threads may prevent the fastener from achieving the required tightening condition.
Manufacturers should inspect critical dimensions and verify that threaded features match the specified thread type and size. Where applicable, thread gauges can be used to check thread conformity.
For products using separate nuts and bolts, the compatibility of the fastening components must also be confirmed. The clamp body, bolts, nuts, and washers should be selected and assembled according to the product design and application requirements.
Surface treatment helps protect bolted clamps from corrosion, improves appearance, and supports the intended service life. The appropriate finishing process depends on the base material and operating environment.
Stainless steel clamps may undergo deburring, cleaning, pickling, passivation, or polishing, depending on the required surface condition. These processes can help remove contaminants, improve surface cleanliness, and support corrosion resistance when properly specified and performed.
Carbon steel clamps may require galvanizing, electroplating, painting, or other protective coatings. The coating type and thickness should be selected according to the expected exposure conditions and applicable requirements.
Surface inspection should identify sharp edges, burrs, visible cracks, coating defects, and other imperfections that could affect installation or performance. For applications with strict cleanliness requirements, buyers should also specify acceptable surface conditions and any restrictions on finishing materials.
Bolts are critical components of a bolted clamp assembly because they help secure the clamp and maintain the required connection. Their performance depends on material grade, diameter, thread specifications, length, and tightening requirements.
Manufacturers should select fasteners that meet the specified mechanical properties and environmental requirements. In corrosive environments, fastener material compatibility is especially important. Using dissimilar metals without considering galvanic corrosion may lead to premature deterioration under certain conditions.
The tightening method should also be appropriate for the design. Insufficient tightening may allow movement or loosening, while excessive tightening can damage threads, deform clamp components, or compromise the assembly.
Where the application requires controlled preload or a specified tightening torque, the manufacturer should define the relevant requirements and verify assembly procedures. The correct torque should come from the applicable design or engineering specification rather than a universal value.
Dimensional inspection is an essential part of bolted clamp quality control. Manufacturers need to confirm that finished components match the approved drawings and fit the intended installation conditions.
Common inspection points include:
Clamp inner diameter or clamping range
Overall length, width, height, and material thickness
Hole diameter, spacing, and alignment
Thread size and condition
Bolt length and fastening compatibility
Component alignment and assembled fit
Depending on the required tolerance, inspection tools may include calipers, micrometers, height gauges, thread gauges, and dedicated inspection fixtures.
Assembly verification checks whether the clamp components fit together correctly and whether the fasteners can be installed without interference. For clamps designed around a specific pipe size or mounting configuration, a fit test using a reference component may help confirm compatibility.
The type and extent of mechanical testing depend on the clamp’s intended use and the risks associated with failure. Not every bolted clamp requires the same test program.
For load-bearing or heavy-duty applications, manufacturers may perform load tests to verify that the clamp withstands specified forces without unacceptable deformation or failure. Test conditions should reflect the design requirements and the expected direction of loading.
Functional testing may also assess whether the clamp can be installed, tightened, opened, or removed as intended. Where the product is designed to resist movement, slipping, or vibration, additional testing may be required under defined conditions.
For clamps used in pressure-containing or safety-critical assemblies, testing should follow the applicable product specification and engineering requirements. Buyers should confirm which tests are included, the acceptance criteria, and whether test reports are available.
Corrosion resistance is an important consideration for bolted clamps used outdoors, in humid environments, or in contact with corrosive substances. The required protection depends on the base material, surface finish, and service conditions.
For stainless steel clamps, material verification and appropriate surface treatment help ensure that the selected grade and finishing process meet the specified requirements. For coated carbon steel clamps, coating thickness measurements and coating adhesion checks may be relevant.
Salt spray testing may be specified for certain coated products to evaluate their resistance to a controlled corrosive environment. However, salt spray results do not directly predict the exact service life of a clamp in every real-world environment.
Visual inspection should also check for rust, pitting, scratches, coating damage, discoloration, and other surface defects. The acceptance criteria should be defined according to the product specification and intended application.
Before shipment, manufacturers should carry out a final inspection to confirm that the finished bolted clamps meet the order requirements. This may include reviewing dimensions, materials, fastener specifications, surface finish, assembly condition, and quantity.
For projects requiring traceability, manufacturers may provide material certificates, inspection reports, batch numbers, or other quality records. These documents help buyers verify product conformity and support quality management throughout the supply chain.
Packaging is another important consideration, especially for export orders. Clamps should be packed to reduce the risk of scratches, deformation, moisture exposure, and damage during transportation. Bolts, nuts, washers, and other accessories should be organized to prevent loss or mixing between product specifications.
Clear product labels and packaging records can also help distributors, installers, and end users identify the correct components after delivery.
Selecting a qualified manufacturer requires more than comparing unit prices. Buyers should assess the supplier’s ability to maintain consistent quality, meet technical specifications, and support the required order volume.
First, confirm that the manufacturer has experience producing the specific type of bolted clamp required. Different designs may involve different forming processes, machining capabilities, fastener requirements, and inspection methods.
Second, review the supplier’s quality control procedures. Ask how incoming materials are verified, which dimensions are inspected, how fasteners are checked, and what testing is available for the intended application. Relevant material certificates and inspection reports can provide additional evidence of product conformity.
Third, confirm the manufacturer’s customization capabilities. Depending on production capacity, customization may include dimensions, material grades, bolt specifications, surface treatments, packaging, and product marking. Buyers should provide technical drawings or detailed requirements to reduce the risk of manufacturing errors.
Finally, evaluate lead times, minimum order quantities, communication efficiency, and export packaging. A dependable supplier should be able to explain its manufacturing process, clarify technical requirements, and provide documentation appropriate to the order.
Bolted clamp manufacturing involves several important stages, including material selection, cutting and forming, hole and thread processing, surface finishing, fastener selection, dimensional inspection, and final quality verification. Each stage can affect the clamp’s fit, mechanical performance, corrosion resistance, and service life.
For industrial buyers, quality testing should be matched to the product’s design and intended application. Dimensional checks, material verification, assembly inspection, and appropriate mechanical or corrosion testing help confirm that the clamp meets its specified requirements.
By evaluating manufacturing capabilities, inspection procedures, material traceability, and customization options, buyers can choose a reliable bolted clamp manufacturer and reduce the risk of installation problems or premature product failure.
1. What materials are commonly used to manufacture bolted clamps?
Bolted clamps are commonly manufactured from stainless steel, carbon steel, and other metals suitable for the intended application. Stainless steel grades such as 304 and 316 are often selected for corrosion resistance, while carbon steel may be used for applications requiring strength and cost-effective production.
2. What are the main manufacturing processes for bolted clamps?
The manufacturing process typically includes raw material preparation, cutting, forming or machining, drilling or punching, thread processing, surface treatment, and assembly. The exact process depends on the clamp design, material, production volume, and dimensional requirements.
3. How are bolted clamps tested for quality?
Quality testing may include dimensional inspection, material verification, thread inspection, visual examination, assembly checks, and surface finish evaluation. Depending on the application, manufacturers may also conduct load testing, functional testing, coating thickness measurement, or corrosion resistance testing.
4. Why is dimensional inspection important for bolted clamps?
Dimensional inspection ensures that the clamp fits the intended pipe, component, or mounting surface. Checking the clamping diameter, material thickness, hole spacing, thread specifications, and overall dimensions helps prevent installation difficulties and compatibility issues.
5. How do manufacturers verify the quality of bolts used in bolted clamps?
Manufacturers verify fastener quality by checking material specifications, bolt dimensions, thread compatibility, and required mechanical properties. For critical applications, additional inspection or testing may be necessary to confirm that the fasteners meet the relevant specifications.
STAINLESS STEEL&GENCEL;
Privacy Policy | SiteMap
Copyright GENCEL STAINLESS STEEL CO.,LIMITED
 Optimized by Seraphinite Accelerator