- Whatsapp: 8613738300923
- Email: [email protected]


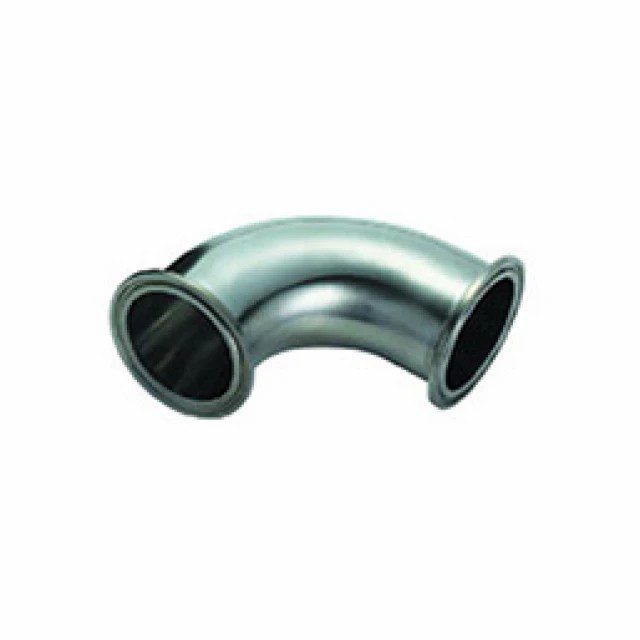
A 90 degree stainless steel elbow is an essential pipe fitting used to change the direction of flow by 90 degrees in industrial piping systems. These fittings are widely used in chemical processing, oil and gas, water treatment, food and beverage production, pharmaceutical manufacturing, and other industries that require reliable and corrosion-resistant pipe connections.
The quality of a stainless steel elbow depends on several factors, including material selection, forming technology, dimensional accuracy, wall thickness control, and inspection procedures. Poor manufacturing quality can lead to dimensional inconsistencies, surface defects, or reduced performance under demanding operating conditions.
Understanding how 90 degree stainless steel elbows are manufactured and quality tested helps buyers evaluate suppliers, compare products, and select fittings that meet their technical requirements.
Material selection is the first step in manufacturing a high-quality 90 degree stainless steel elbow. The material must provide suitable corrosion resistance, mechanical strength, and formability for the intended application.
Common stainless steel grades include 304, 304L, 316, and 316L. Grade 304 is widely used in general industrial piping systems because of its versatility and corrosion resistance. Grades 316 and 316L contain molybdenum, which improves resistance to certain corrosive environments, including many chloride-containing conditions. However, actual performance depends on the concentration of the medium, temperature, and operating conditions.
Manufacturers may use stainless steel seamless pipe, welded pipe, or other suitable starting materials depending on the product specification and manufacturing method. Before production, incoming materials should be checked against the required grade and applicable material standards.
Material certificates, heat numbers, and additional material identification tests may be used to verify compliance. Proper material control helps prevent incorrect grades from entering production and supports traceability throughout the manufacturing process.
After material verification, the stainless steel starting material is prepared according to the required elbow dimensions and manufacturing process.
Preparation may involve cutting the pipe to the required length, checking its outside diameter and wall thickness, and inspecting the surface for visible defects. The starting material must be suitable for the intended forming operation.
Incorrect dimensions or inconsistent material properties can affect the final elbow geometry. For example, unsuitable starting wall thickness may result in excessive thinning at certain locations during forming.
Manufacturers should establish clear material preparation procedures and inspect critical dimensions before forming begins. This helps reduce production defects and improve consistency between batches.
Forming is one of the most important stages in elbow manufacturing. The selected process depends on the elbow diameter, wall thickness, material grade, bend radius, production volume, and applicable product requirements.
Common manufacturing methods include hot forming, cold forming, and induction bending for suitable product designs.
Hot forming uses elevated temperatures to improve material formability during shaping. It is commonly used for certain elbow sizes and geometries that require substantial deformation.
Cold forming shapes the material without heating it to high forming temperatures. Depending on the process and material, it can provide good dimensional control and surface quality, although forming forces and work hardening must be considered.
Induction bending uses localized heating and mechanical force to bend suitable pipe sections along a specified radius. It is generally associated with larger or specialized pipe bends and should not be confused with every conventional short-radius or long-radius elbow manufacturing process.
For standard butt-weld elbows, manufacturers may also use dedicated forming equipment and tooling to achieve the required 90-degree angle and curvature. Process parameters must be controlled to minimize cracking, wrinkling, excessive thinning, and other forming defects.
The bend radius and wall thickness directly influence the dimensions and performance of a 90 degree stainless steel elbow.
Long-radius elbows generally have a centerline radius of 1.5 times the nominal pipe size, while short-radius elbows generally have a centerline radius equal to the nominal pipe size. The exact dimensional definitions should be confirmed against the applicable standard and nominal pipe size system.
During forming, the material on the outside of the bend is subjected to tensile deformation, while the inside experiences compressive deformation. These forces can cause wall thinning, thickening, or distortion if the manufacturing process is not properly controlled.
Manufacturers should inspect critical dimensions, including the bend angle, center-to-end dimensions, outside diameter, and wall thickness. Additional measurements may be necessary for specialized designs or demanding applications.
Consistent control of these parameters helps ensure that the finished elbow fits the piping system and meets the applicable dimensional requirements.
After forming, the elbow may undergo trimming and end preparation to achieve the required dimensions and connection geometry.
For butt-weld elbows, the ends must be prepared according to the relevant design and installation requirements. Bevel angle, end diameter, and other critical dimensions should be checked before the fitting is approved for shipment.
Surface finishing may include mechanical polishing, pickling, passivation, or other suitable treatments. The selected treatment depends on the material condition, product specification, and intended application.
Pickling can help remove oxide scale and certain surface contaminants generated during manufacturing. Passivation supports the formation of the protective passive film under appropriate conditions. Neither process replaces the need for a suitable stainless steel grade or proper corrosion control.
For sanitary and hygienic applications, buyers may require specific surface roughness, cleanliness, or finishing procedures. These requirements should be clearly defined before production.
Dimensional inspection verifies that the finished 90 degree stainless steel elbow meets the specified geometry and tolerances.
Important inspection parameters may include:
Bend angle and center-to-end dimensions
Outside diameter and wall thickness
Bend radius and overall geometry
End diameter and bevel dimensions
Ovality and visible deformation
Surface condition and manufacturing defects
Manufacturers may use calibrated measuring instruments, gauges, templates, and dedicated inspection fixtures to check these parameters.
The acceptance criteria should be based on the applicable product standard, approved drawings, and purchase specifications. Buyers should not assume that every elbow follows the same dimensional tolerances, particularly when comparing different sizes, schedules, or manufacturing methods.
Dimensional inspection helps reduce installation problems and ensures compatibility with the intended piping system.
Material verification confirms that the elbow meets the specified stainless steel grade and applicable material requirements.
Manufacturers may review material test certificates and, when required, conduct positive material identification (PMI) or other appropriate checks. These procedures help verify alloy composition and maintain traceability between the raw material and finished product.
Mechanical testing may include tensile testing, hardness testing, or other examinations specified by the applicable material standard. The required tests depend on the starting material, manufacturing process, product specification, and contractual requirements.
For certain formed products, additional evaluation may be necessary to confirm that the manufacturing process has not adversely affected the required material properties.
A reliable manufacturer should maintain appropriate inspection records and make the required documentation available to buyers. Testing should follow the applicable specification rather than relying on a universal checklist for all elbow products.
Non-destructive testing (NDT) may be required to identify defects without damaging the finished elbow. The appropriate inspection method depends on the product design, manufacturing process, material, and intended service.
Common methods include:
Liquid penetrant testing: Used to identify surface-breaking discontinuities on suitable nonporous surfaces.
Radiographic testing: Uses radiation to detect certain internal defects in suitable components and configurations.
Ultrasonic testing: Uses high-frequency sound waves to detect certain internal discontinuities or evaluate material thickness.
Visual testing: Helps identify visible surface defects, forming irregularities, and other signs of poor workmanship.
Not every 90 degree stainless steel elbow requires every NDT method. The inspection method, testing extent, and acceptance criteria should be determined by the relevant standard, engineering requirements, and purchase agreement.
For welded starting materials or specialized fittings, additional weld-related inspections may be necessary where specified. Inspection records should identify the product or batch and document the required results.
International standards help establish consistent requirements for materials, dimensions, manufacturing, and inspection. The appropriate standard depends on the type of elbow, manufacturing method, material grade, and intended application.
Commonly referenced standards include:
ASME B16.9: Covers factory-made wrought butt-welding fittings, including applicable 90 degree elbows. It addresses dimensions, tolerances, ratings, testing, and marking requirements within its scope.
ASTM A403/A403M: Covers wrought austenitic stainless steel piping fittings for pressure piping applications. It specifies material and related requirements for fittings within its scope.
ASME B36.19M: Specifies dimensions and schedules for stainless steel pipe. It may be relevant when confirming the dimensions of the connected piping, but it is not a substitute for the applicable elbow fitting standard.
Buyers should confirm the applicable standard and edition before ordering. They should also verify that the product’s material grade, nominal size, wall thickness, pressure-temperature requirements, and inspection documentation match the project specification.
A manufacturer should clearly state which standards apply to its products and provide supporting documents when required.
Before shipment, finished elbows should undergo final inspection to confirm that they meet the agreed product specifications.
Final inspection may include dimensional verification, visual examination, review of required test records, and confirmation of material identification. Depending on the order, the manufacturer may also check marking, quantity, packaging, and documentation.
Product markings may include information such as material grade, nominal size, wall thickness or schedule, manufacturer’s identification, and applicable specification details, subject to the relevant standard and customer requirements.
Packaging should protect the elbow surfaces and ends during handling, storage, and transportation. Stainless steel fittings should be handled and packed in a way that reduces contamination, scratches, deformation, and damage to prepared ends.
For export orders, buyers should confirm packaging requirements, identification methods, and the documents that will accompany the shipment before production is completed.
Understanding the manufacturing process is useful, but buyers should also evaluate whether a manufacturer can consistently meet the required quality standards.
When assessing a supplier, consider the following factors:
Material control: Confirm whether the manufacturer can provide appropriate material certificates and maintain traceability.
Manufacturing capabilities: Check whether the factory can produce the required sizes, wall thicknesses, bend radii, and stainless steel grades.
Quality inspection: Ask about dimensional inspection, surface examination, mechanical testing, and any required NDT procedures.
Standards compliance: Verify which product standards apply and request technical datasheets or sample inspection reports.
Customization and delivery: Confirm whether the manufacturer can meet special dimensions, finishing requirements, packaging specifications, and delivery schedules.
Quality documentation: Establish which certificates and inspection records will be supplied with the order.
For large or critical projects, buyers may consider a factory audit, third-party inspection, or agreed witness testing. These measures provide additional assurance that the delivered products meet the contractual requirements.
Manufacturing a high-quality 90 degree stainless steel elbow requires suitable raw materials, controlled forming processes, accurate dimensional inspection, proper surface finishing, and appropriate quality testing. Wall thickness, bend radius, material properties, and end preparation must all meet the requirements of the intended piping system.
Standards such as ASME B16.9 and ASTM A403/A403M provide important guidance for applicable wrought butt-weld stainless steel elbows. However, the exact standards and testing requirements depend on the product design, application, and purchase specifications.
For distributors, contractors, and industrial buyers, evaluating manufacturing capabilities alongside material certificates, inspection procedures, and traceability records is essential. A reliable stainless steel elbow manufacturer should be able to demonstrate that its products meet the agreed technical requirements and provide consistent quality across production batches.
STAINLESS STEEL&GENCEL;
Privacy Policy | SiteMap
Copyright GENCEL STAINLESS STEEL CO.,LIMITED
 Optimized by Seraphinite Accelerator